

Updated: October 2026
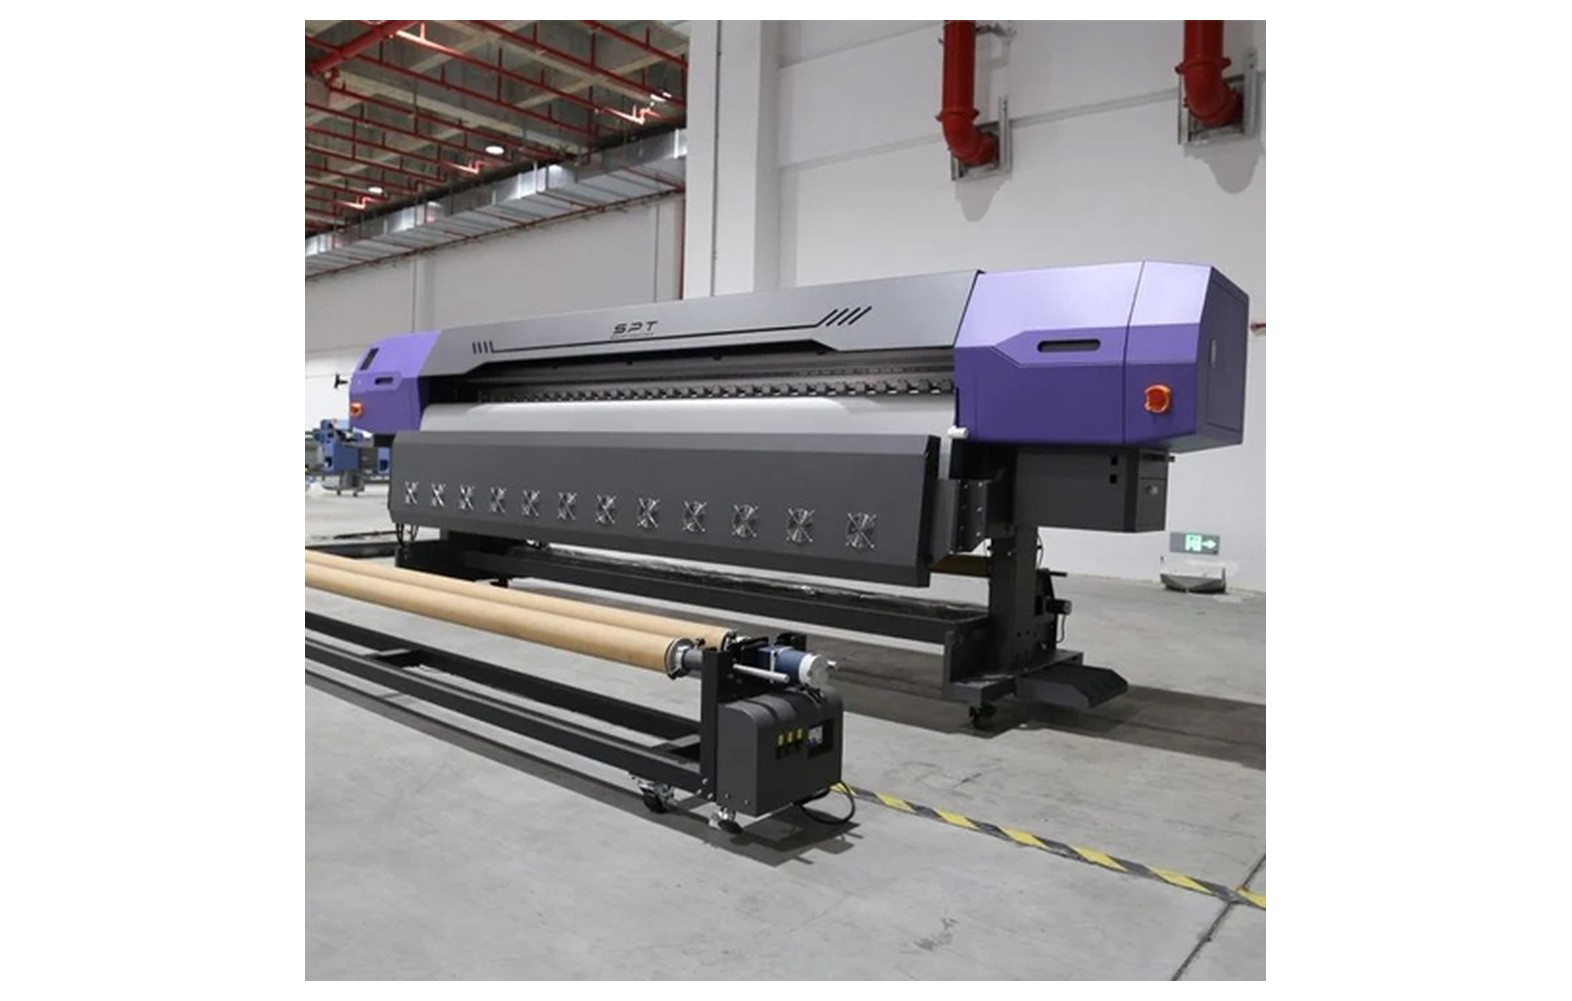
Every 16 ft flex plant meets the same fifteen failures – usually at 11 PM with a launch deadline breathing down the shed. Knowing the order of suspects turns a 3-day service wait into a 20-minute fix you perform yourself. This guide lists the fifteen problems, their usual causes and the fixes that work, in the sequence an experienced operator walks. All figures are estimates (est.).
The 15 Problems, Causes and Fixes
| # | Problem | Usual cause | Fix |
|---|---|---|---|
| 1 | Banding lines across print | nozzle decline, dirty encoder, worn rail, voltage sag | nozzle test, clean encoder, rail check, then power audit |
| 2 | Head clogs returning daily | dry cap tops, old filters, mixed ink brands | cap-top and filter service, single ink brand, flush soak |
| 3 | Colors differ from last month | new media lot, profile drift, temperature swing | re-linearize and profile per media lot, log room temps |
| 4 | Print misaligned left-right over 5 m | media feed drift, pinch pressure uneven | re-set pinch pressure, calibrate feed, check roll loading |
| 5 | Ink wet at wind-up, smudging | heater zone dead, speed too high for cure profile | thermometer each zone, slow to cured profile, IR assist |
| 6 | Media skews and wrinkles mid-roll | roll loaded loose, dancer arm sticky, floor not level | reload tight, free the dancer, re-level |
| 7 | Random carriage stops mid-print | overheating drivers, cable wear, static | cooling fans first, drag-chain cables, earthing check |
| 8 | Misting, overspray haze around print | head too high, voltage too high, static charge | re-gap heads, tune head voltage, humidify in dry winters |
| 9 | Print fades on hoarding in months | economy ink, wrong media grade for exposure | grade-up ink and frontlit for exposed sites, laminate premium |
| 10 | Head strike scratches across media | media edge curled, head height too low, warped roll | trim roll edges, raise gap on thick media, replace warped rolls |
| 11 | Feed motor errors, take-up slip | dancer sensor, motor driver heat, tension settings | sensor clean, cool cabinet, tension re-learn on roll class |
| 12 | RIP software crash or dongle missing | USB port wear, Windows update, driver loss | dedicated print PC offline, dongle spare plan, driver pack saved |
| 13 | Bubbles and fish-eyes in solid colors | mixing ink batches, wet media, contaminant in line | same-batch rule, dry media storage, line flush |
| 14 | Edges print lighter than centre | carriage height drift with media sag, platen heat uneven | vacuum section check, platen zones tuned to media width |
| 15 | Total power trip during heater cycles | undersized line, heater element aging, loose lugs oxidized | electrician: upsize line, torque and clean all lugs, test elements |
The 20-Minute Daily Prevention Routine
| Minute | Ritual | Kills problems |
|---|---|---|
| 0-5 | nozzle test pattern, log it | 1, 2 |
| 5-10 | head face swab, cap-top check, wiper clean | 2, 8 |
| 10-13 | encoder strip wipe | 1 |
| 13-17 | heater zone check with thermometer | 5 |
| 17-20 | media loading and pinch pressure sanity check | 4, 6, 10 |
Fix-Yourself vs Call-Service Line
- DIY zone: cleaning rituals, media handling, pinch pressure, encoder, filters, profiles, heater zones – twelve of these fifteen live here.
- Call service: mainboard and driver faults, head replacement with voltage tuning, carriage rebuilds, persistent electrical trips – document errors with photos before the call.
- Keep one trained-operator habit sacred: fault diary with date, symptom and action – three months of entries predict service calls before they happen.
Our Verdict
Ninety percent of these fifteen die inside the 20-minute daily ritual; the rest die inside a spares shelf holding filters, wipers, cap-tops and one spare head (est. Rs 60,000-1 lakh shelf). Downtime in hoarding season is the only truly expensive problem. See plant spares planning inside the Rs 2 Cr flex hoarding plant case study, browse flex printing machines, and prevent with the all-India printing business startup guide.
FAQs – 15 Common Flex Machine Problems and Fixes 2026
Why is my flex machine showing banding lines?
Work the ladder: nozzle test first for declining heads, then wipe the encoder strip, check carriage rail for wear spots, and audit voltage sag during heater cycles (est.). Ninety percent of banding resolves in these four checks before any part needs replacing.
How do I fix head clogs on a solvent flex printer?
Panel clean cycle, then moist cap rest, then syringe flush through the head face if stubborn (est.). Daily clogs signal deeper causes: drying cap tops, old ink filters or mixed ink brands – fix those and the clogs stop returning.
Why does flex print color change between batches?
Media lot changes, RIP profile drift and room temperature swings shift printed color (est.). Re-linearize and re-profile for each new media roll lot, keep profiles named per media, and log shop temperatures across seasons.
What causes ink to stay wet and smudge at wind-up?
Curing shortfall: a dead heater zone, print speed above the cure profile, or insufficient dry distance. Thermometer-test all platen zones, slow to the media’s cured profile, and add IR assist for heavy-coverage premium work (est.).
More 16 ft flex printing machine guides: 16 Feet Flex Machine Price Guide 2026, 10 ft vs 16 ft Flex Machine, Hoarding Printing Business Guide, Konica 512i vs 1024i Printheads, 16 ft Flex Machine Running Cost, Star Flex vs Normal Flex Difference, 16 ft Flex Machine Installation Guide, Flex Printing Materials and Rates, 16 ft Flex Machine Maintenance Schedule, 16 ft Flex Plant ROI Case Study, Second-Hand 16 ft Flex Machine Checklist, Building Wrap and Facade Printing Guide, 16 ft Flex vs UV Roll-to-Roll, Unipole and Trivision Hoarding Guide.
Share your hoarding sizes and target buyers on the contact page – we reply with an exact machine quote, freight and installation plan for your city, with on-site training across India.
