

Updated: October 2026
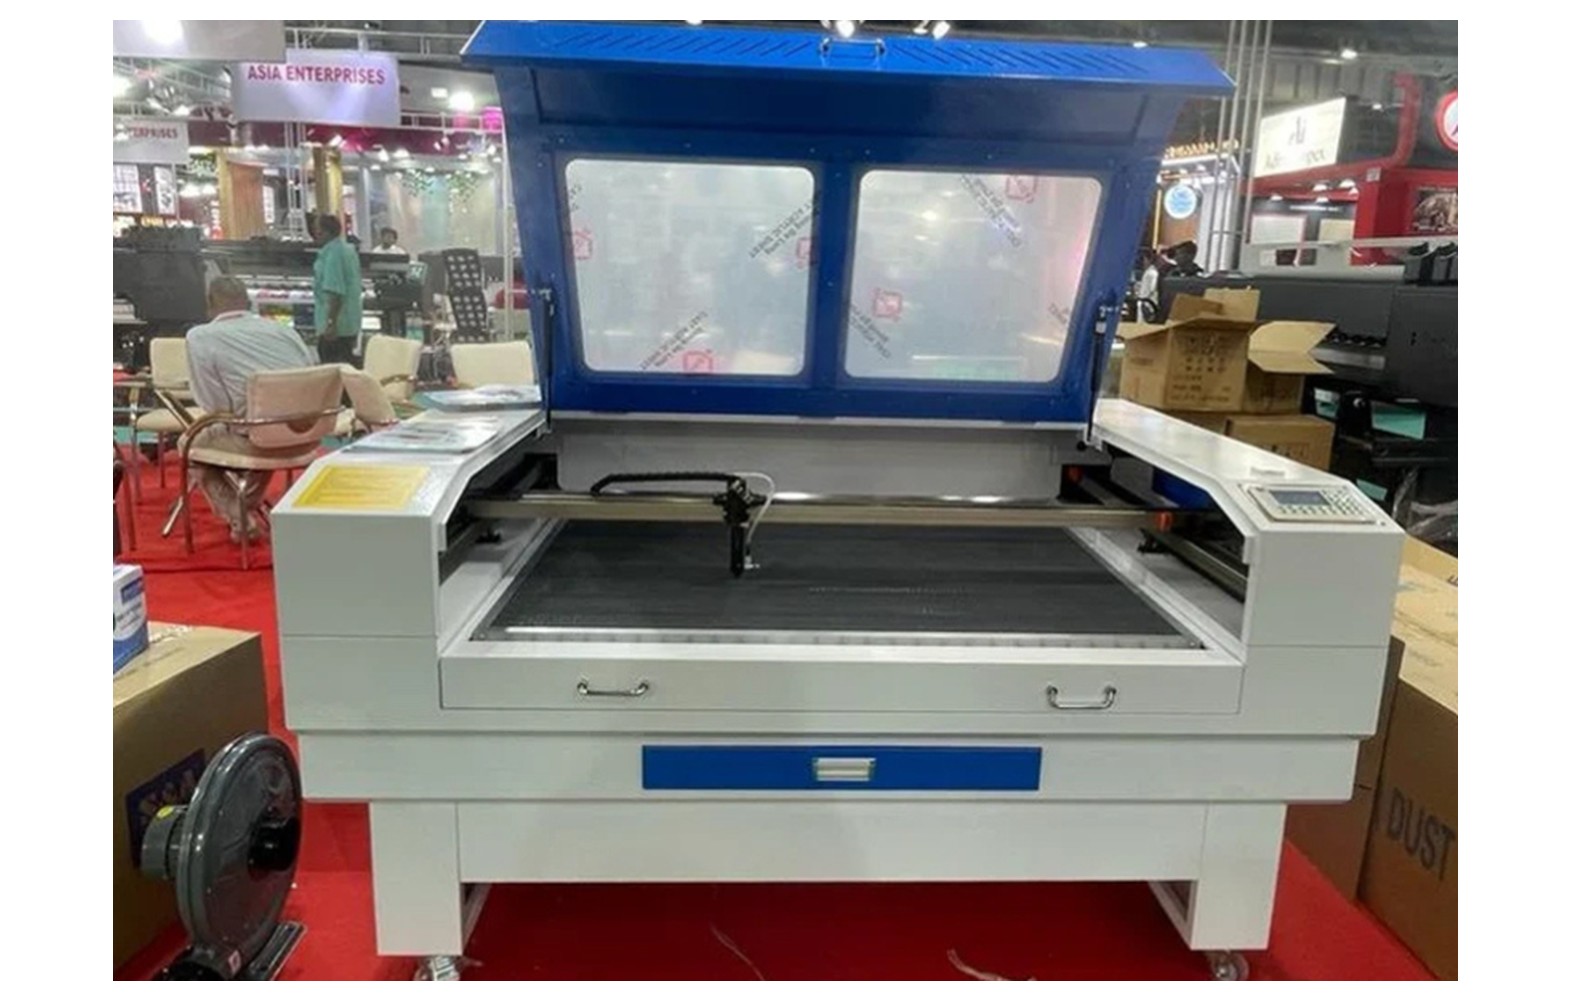
Acrylic is the CO2 laser’s superpower – polished, sealed edges straight off the bed. But PMMA punishes lazy settings with flames, taper and cloudy engraving. This guide gives a practical starting chart for 100W-class machines, the cast-versus-extruded truth, and fixes for the six defects that waste sheets. All speed and power values are starting estimates (est.) – every tube drifts, so tune with test squares before production runs.
Acrylic Cutting Settings Chart, 100W Reference (est.)
| Thickness | Speed | Power | Air assist | Focus |
|---|---|---|---|---|
| 2 mm | 25-30 mm per second | 55-65% | low | surface |
| 3 mm | 18-22 mm per second | 60-70% | low | surface |
| 4 mm | 14-18 mm per second | 65-75% | low | surface |
| 5 mm | 10-14 mm per second | 70-80% | low-medium | 1 mm into sheet |
| 6 mm | 8-10 mm per second | 75-85% | low-medium | 2 mm into sheet |
| 8 mm | 5-7 mm per second | 80-90% | medium | 2-3 mm into sheet |
| 10 mm | 3-5 mm per second | 85-95% | medium | 3 mm into sheet |
| 12 mm | 2-3 mm per second | 90-100% | medium | 4 mm into sheet |
Adjustment notes: a healthy 150W tube runs these jobs about 25-30% faster or thicker at the same speeds. Losing power mid-sheet is the classic sign of a warm tube – check chiller temperature before touching speed.
Cast vs Extruded Acrylic
| Property | Cast acrylic | Extruded acrylic |
|---|---|---|
| Cut edge finish | Excellent, clean and glossy | Good, slight striations possible |
| Engraving | Frosty white contrast – ideal for awards | Weak, clearish marks |
| Heat stress and cracking | More resistant | Crazes easily under poor settings |
| Price behaviour (est.) | 15-25% costlier | Cheaper, wider size availability |
| Best use | Trophies, engraved panels, displays | Cut letters, boxes, glazing |
Air Assist, Focus and the Flame-Polished Edge
- Low air, always, on acrylic: strong air cools the melt and dulls the edge; just enough pressure to stop flames licking upwind.
- Focus into the sheet above 5 mm: focusing one-third of the thickness deep keeps the kerf parallel instead of tapered.
- Flame-polished edges are a speed-power game: one decisive pass at full rated speed for the thickness; crawling reheats and frosts the edge.
- Keep the honeycomb clean: residue flashes back marks on the sheet underside; knife beds beat honeycomb for acrylic letters.
Masking and Handling
- Paper masking beats plastic film: it peels without crazing and does not melt into the kerf.
- Never wipe fresh-cut acrylic with thinner; use isopropyl alcohol sparingly – aggressive solvents cause stress cracks within hours.
- Let hot sheets rest flat for 20-30 minutes before de-mask and assembly to avoid warping thin pieces.
Troubleshooting the 6 Common Acrylic Defects
| Defect | Cause | Fix |
|---|---|---|
| Flames during cutting | air too low or none, power too low for speed | raise air slightly, increase speed or power, never leave machine unattended |
| Tapered or wedge edge | focus at surface on thick sheet | focus one-third depth into material |
| Cloudy, unclear engraving | too much power, extruded sheet | lower power, raise speed, use cast acrylic |
| Grid marks on underside | dirty honeycomb reflection | clean bed, raise sheet 3-5 mm on pins, use knife bed |
| Stress cracks after days | solvent exposure, tight mechanical fits | no aggressive solvents, allow 0.2-0.3 mm fit clearance |
| Bottom not cut through | tube ageing, focus drift, dirty lens | clean optics, refocus, check tube current against rating |
Our Verdict
Master this chart on one machine before blaming the next – 90% of acrylic complaints are focus, air or optics, not the tube. Stock cast sheets for engraved awards and extruded for cut letters, keep extraction steady with a real dust collectors, and see the volume economics inside the Rs 1 Cr trophy and marking factory case study and Rs 1 Cr corporate gift plant case study. Browse CO2 laser machines for machines sized to acrylic work, and plan staging with the all-India printing business startup guide.
FAQs – Acrylic Laser Cutting Settings Chart India 2026
What are the best settings to cut 6 mm acrylic with a 100W CO2 laser?
Start at 8-10 mm per second, 75-85% power, low-medium air assist and focus 2 mm into the sheet (est.). Tune one test square: faster for glossy edges, slower only if the bottom misses.
Why does my acrylic keep catching fire?
Flames mean combustible vapours pooling – usually zero or too-weak air assist or a focussing fault that heats a wide kerf. Raise air just until flames die, keep the bed clean and never walk away from a running laser.
Which acrylic is better for engraved trophies – cast or extruded?
Cast acrylic, clearly: it engraves with the frosty white contrast buyers expect on awards. Extruded sheets engrave faint and craze easily under heat.
Can a CO2 laser cut 20 mm acrylic?
Only with 250-300W-class industrial tubes, slow passes and careful focus – and edge quality still falls short of CNC-routed and flame-polished 20 mm work. That thickness is router territory for professional output.
More laser and CNC machine guides: CO2 Laser Machine Price Guide 2026, CNC Router Machine Price Guide 2026, Fiber Marking Machine Price Guide 2026, Laser Engraving Business Ideas, CNC Router Business Ideas, CO2 Laser vs CNC Router, CO2 Laser Wattage Guide, MDF Jali Cutting Business Guide, CO2 Laser Tube Life and Replacement Guide, CNC Router Bits Guide, 12 Common CO2 Laser Problems and Fixes, CNC Router Maintenance Schedule, Dust Collector and Fume Extractor Guide, CO2 Laser Materials Chart, CO2 Laser Speed and Power Settings Chart, ACP Grooving and Cutting CNC Guide, Stone CNC Router Guide, CO2 Laser Chiller Setup Guide, Galvo Laser vs Bed Laser, Laser Home Business Starter Guide, Chinese vs Indian Laser Machines, ATC CNC Router Upgrade Guide, CO2 Laser Rotary Attachment Guide, CNC Router Vacuum Table Guide, Stone Jali vs MDF Jali: Rates and Margins, CO2 Laser Installation and First Week Checklist, CNC Router File Formats Explained, CO2 Laser Lens and Mirrors Guide, CNC Router vs Plasma Cutter.
Share your material, thickness and target buyers on the contact page – we reply with an exact machine quote, freight and installation plan for your city, with on-site training across India.
